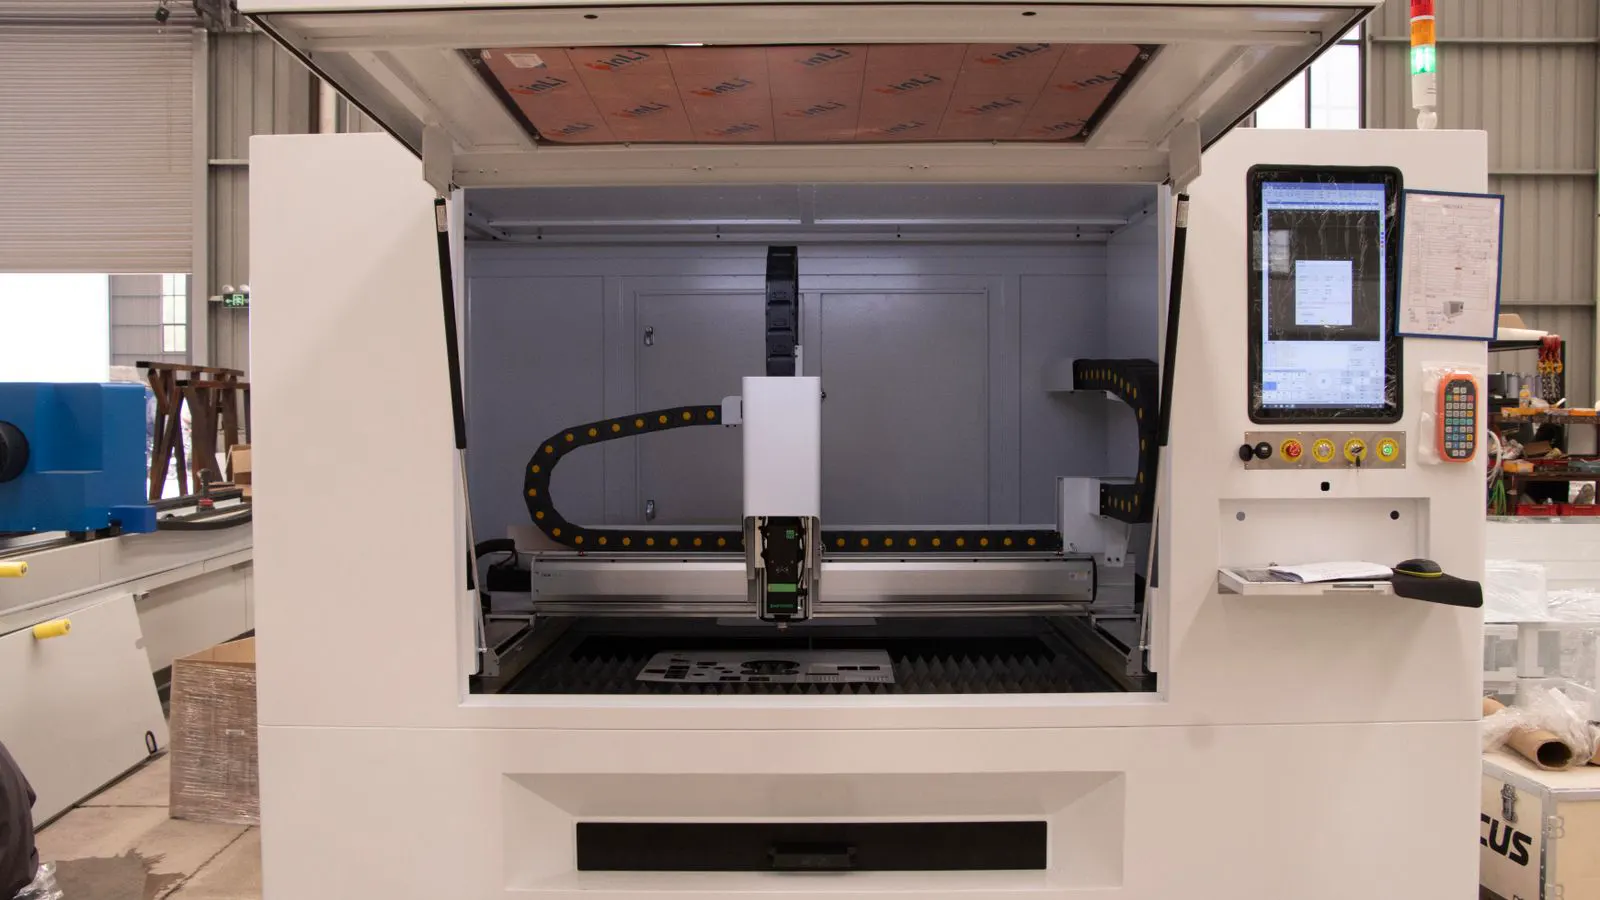
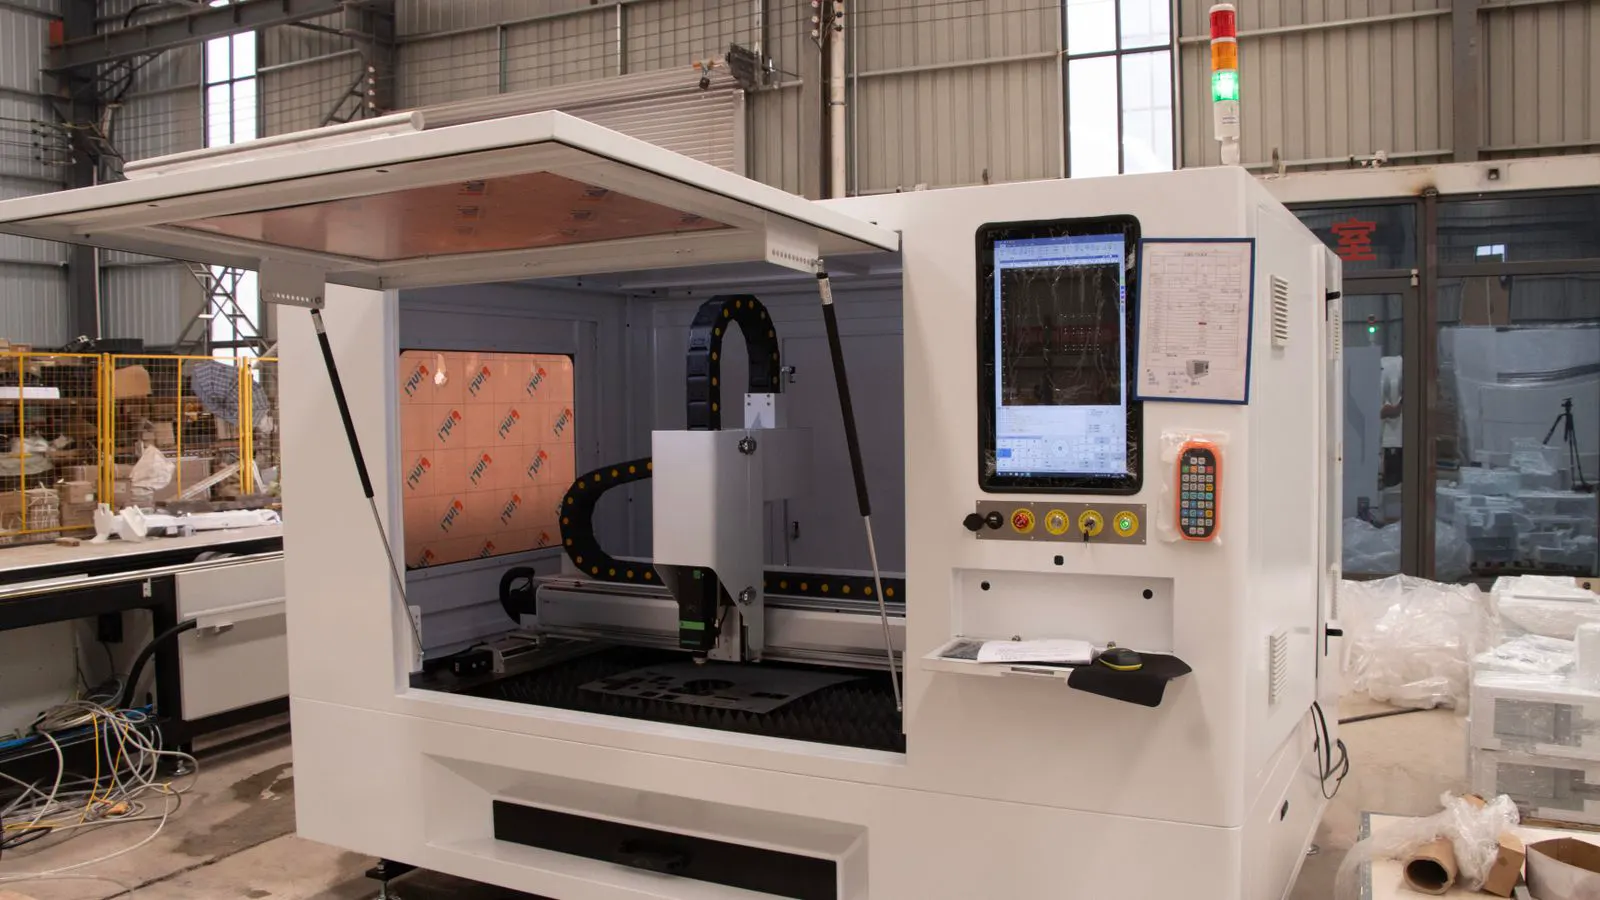
CNC Milling Machine Checklist: 10 Key Specs for Vertical and Horizontal
Use this 10-point checklist to verify critical specs for vertical and horizontal CNC mills. It covers travel, rigidity, spindle, tool changer, and controller checks to help you evaluate machine capability and avoid common evaluation mistakes.
- Verify linear travel and axis overlap to confirm the machine can handle part size and fixture requirements before you commit.
- Inspect spindle load capacity, tool changer, and controller options to match the specific parts and materials you will run.
- Watch for red flags such as limited axis overlap, low spindle load ratings, and missing documentation.
- Use a structured checklist to compare vertical and horizontal mills objectively during the evaluation process.
Start with part size and fixture space
Before looking at spindle RPM or controller features, check linear travel. The X, Y, and Z travel dimensions determine what physical workpiece fits in the machine. A part that barely fits in the raw envelope will likely fail once you add the vise, fixture, tool overhang, and safety clearance.
For vertical mills, the Z-axis travel often limits the maximum part height. If the table sits low or the spindle has limited down travel, the usable Z range can be smaller than the manufacturer’s published figure. Measure the distance from the table surface to the lowest spindle position, and add clearance for the workpiece.
For horizontal mills, the X and Y travel dimensions are often the primary constraints. A horizontal setup usually requires more floor space and a different fixture strategy. If you are machining a long shaft or a wide plate, the horizontal axis travel may be the deciding factor.
Checklist item 1: Linear travel dimensions
- X, Y, and Z travel in millimeters or inches
- Usable work envelope after fixture and tool clearance
- Table size and load capacity
- Axis overlap, if available
Red flag: The published travel matches the part size with no room for fixture, tool overhang, or operator access. If the part fits exactly, the machine is not a fit.
Verify rigidity and structure
Rigidity determines how well the machine holds position under cutting forces. A machine that vibrates or deflects under load will produce poor surface finish, inaccurate dimensions, and accelerated tool wear.
Look for the machine structure type. A monolithic or integrated design, where the spindle head, table, and base are built as a single unit, generally resists deflection better than a frame-and-spindle design. The material matters too. Cast iron is common for its damping characteristics. Aluminum or composite structures can be lighter and faster, but they require careful design to control vibration.
Check the table and ways. A heavy table with long rails and proper way covers helps maintain accuracy over time. If the table is thin or the rails are short, expect more deflection when cutting deep pockets or wide slots.
Checklist item 2: Structure and rigidity
- Monolithic or frame design
- Material of the structure (cast iron, aluminum, or composite)
- Table size and rail length
- Way covers and chip management
Red flag: Thin table, short rails, or a frame design that leaves gaps between major structural components. These features can cause deflection under heavy cuts.
Evaluate spindle capacity and tooling
The spindle is the heart of the machine. Its load capacity, maximum RPM, and tooling compatibility determine what operations you can run.
For general machining, spindle load is more important than maximum RPM. A 10 kW spindle can handle heavier cuts and deeper pockets than a 5 kW spindle with a higher top speed. If you are machining aluminum or plastics, a high-RPM spindle helps with finishing. If you are machining steel, titanium, or hardened materials, spindle torque and load capacity matter more.
Check the spindle taper type. HSK, CAT, or ER collet holders are common. Make sure the machine supports the collets and holders you already use, or plan for new tooling. A tool changer that accepts multiple spindle tapers can save money and setup time.
Checklist item 3: Spindle specifications
- Maximum spindle power in kW or HP
- Maximum RPM and constant torque RPM range
- Spindle taper type
- Tool changer capacity and type
Red flag: A spindle rated for only 3 kW when your parts require heavy roughing, or a tool changer that accepts only one taper type you do not own.
Check tool changer and automation options
The tool changer affects setup time and production flow. A manual tool change is fine for prototyping or low-volume work. For production runs, an automatic tool changer with a sufficient pocket count reduces downtime between operations.
For horizontal mills, the tool changer often sits above the spindle or in a carousel. The pocket count should match the number of tools in your typical job. If you use many drills, end mills, and face mills, a 12-pocket changer may not be enough.
Also check the tool changer speed. A slow changer adds minutes to each setup. If you are running multiple operations in one cycle, the changer speed becomes a bottleneck.
Checklist item 4: Tool changer
- Pocket count
- Changer speed and type (carousel, pallet, or drum)
- Tool compatibility with your existing tooling
- Automatic vs. manual option
Red flag: A 6-pocket changer for a job that requires 15 or more tools, or a changer that cannot accept the tool holders you use.
Review controller and software interface
The controller determines how easy the machine is to program and operate. Most modern CNC mills use Fanuc, Siemens, Heidenhain, or similar controllers. Choose the one your programmers and operators already know.
Check the control’s feature set. Look for canned cycles, macro language, and probing capabilities. If you need automatic part probing or work offset setting, make sure the controller supports it. Some machines include a built-in probe; others require an external unit.
Also check the user interface. A large touchscreen with clear menus and quick-access buttons reduces operator error. If your shop has older operators, a familiar interface can speed up training.
Checklist item 5: Controller and probing
- Controller brand and model
- Canned cycles and macro language
- Built-in or external probing option
- User interface type and screen size
Red flag: A controller that does not support the probing or macro functions you need, or an interface your team has never used.
Compare vertical and horizontal layouts
The orientation of the machine affects setup, tool access, and part handling. A vertical mill has the spindle pointing down. This makes it easier to load and unload parts from the top. It is also easier to use a standard vise.
A horizontal mill has the spindle pointing sideways. This gives better access to the part from the side and can reduce tool overhang. It is often better for through-machining, shaft work, or parts with features on all sides. However, it requires more floor space and often a larger table.
If you are machining a part with deep pockets on one side, a vertical mill may be simpler. If you are machining a shaft with features on multiple surfaces, a horizontal mill may be better.
Checklist item 6: Machine orientation
- Vertical or horizontal
- Table size and load capacity
- Fixture and tool access
- Floor space requirement
Red flag: Choosing a horizontal mill for a simple flat plate part, or a vertical mill for a part that requires access to all four sides without rotation.
Check thermal stability and accuracy
Thermal growth affects dimensional accuracy. As the machine warms up, metal expands. If the machine does not control temperature, part dimensions can drift during a long production run.
Look for thermal compensation options. Some machines include temperature sensors and software that adjusts offsets automatically. Others rely on the operator to warm up the machine for a set period before production.
Accuracy classes are often listed as positional accuracy or repeatability. Lower numbers are better. A machine rated for 10 microns over a long travel range is more accurate than one rated for 20 microns.
Checklist item 7: Thermal stability and accuracy
- Positional and repeatability accuracy
- Thermal compensation option
- Warm-up time before production
- Linear guide type and lubrication
Red flag: No thermal compensation for a machine that will run long production cycles, or accuracy ratings that do not match your part tolerance.
Review documentation and support
A machine without proper documentation is a liability. Before you sign the purchase order, verify that the seller can provide the full set of documents.
You should receive the operating manual, programming manual, maintenance manual, and a parts catalog. These documents should be in a format your team can access. PDF files are standard, but some shops prefer printed copies.
Check the warranty terms. A standard warranty may cover parts and labor for a set period. Extended warranties are available, but they cost more. Read the exclusions carefully. Some warranties do not cover tooling, fixturing, or operator error.
Also verify the service plan. If the machine breaks down, how fast can the vendor respond? A local service center is usually faster than a vendor that requires a long-distance repair team.
Checklist item 8: Documentation and support
- Operating, programming, and maintenance manuals
- Warranty terms and exclusions
- Service response time
- Training included with the purchase
Red flag: Missing manuals, a warranty that excludes common failures, or no local service support.
Build your comparison table
Use this table to compare two or more machines side by side. Fill in the values from the seller’s data sheets and your own calculations. Do not rely only on the marketing brochure. Ask the seller to confirm the numbers in writing.
| Specification | Machine A | Machine B | Machine C |
|---|---|---|---|
| Linear travel (X, Y, Z) | |||
| Spindle power (kW) | |||
| Maximum RPM | |||
| Tool changer pockets | |||
| Controller model | |||
| Table load capacity (kg) | |||
| Positional accuracy | |||
| Orientation (vertical/horizontal) | |||
| Warranty period | |||
| Service response time |
Checklist item 9: Comparison data
- Request data sheets in writing
- Confirm all numbers with the seller
- Include your part dimensions and fixture requirements
- Compare the cost per setup and per part
Red flag: The seller cannot provide a written data sheet, or the numbers in the brochure do not match what the sales engineer says.
Final verification steps
Before you place the order, run a final check. Confirm the machine meets your part size, material, and tolerance requirements. Verify that the tooling you plan to use is compatible with the spindle and tool changer. Make sure the controller matches your programming team’s skills.
If possible, run a test part on the machine. Bring a representative part from your production line. If the seller allows it, have your programmer load a program and run it. This is the fastest way to identify issues that do not show up in a data sheet.
If the machine does not pass the test, walk away. A machine that does not fit your process will create problems that cost more than the machine itself.
Checklist item 10: Final verification
- Test part run
- Written confirmation of specs
- Fixture and tooling compatibility
- Warranty and service agreement
Red flag: The machine cannot run your test part, or the seller will not provide written confirmation of the specifications.
Quick-reference summary
Use this numbered list as a final check before you sign the purchase order.
- Confirm linear travel and usable work envelope.
- Verify structure type and table rigidity.
- Check spindle power, RPM, and taper type.
- Confirm tool changer pocket count and speed.
- Review controller model and probing capability.
- Choose vertical or horizontal based on part access.
- Check thermal stability and accuracy ratings.
- Verify documentation and warranty terms.
- Compare machines in a side-by-side table.
- Run a test part and confirm specs in writing.
Each item on this list takes only a few minutes to check. The time you spend now saves you from a machine that does not fit your work. A CNC mill is a long-term investment. Make sure the specifications match your actual production needs before you commit.
Frequently asked questions
What is the difference between a vertical and a horizontal CNC mill?
A vertical mill has the spindle pointing down, making top loading and standard vise use easier. A horizontal mill has the spindle pointing sideways, which improves access to part features and reduces tool overhang.
How do I know if a CNC mill is rigid enough for my parts?
Look at the structure type, table size, rail length, and material. A monolithic design with a heavy table and long rails generally resists deflection better than a light frame design.
Should I prioritize spindle RPM or spindle power?
It depends on the material. For aluminum and plastics, high RPM helps with finishing. For steel, titanium, or heavy roughing, spindle torque and load capacity matter more.
What documents should I request before buying a CNC mill?
Request the operating manual, programming manual, maintenance manual, parts catalog, and a written data sheet with all specifications.
How many tool changer pockets do I need?
Count the tools in your typical job and add a margin for changeovers and breakage. If you use 15 or more tools per setup, a 12-pocket changer may not be enough.